
How to Optimize Your Alu Alu Blister Packaging Line for Zero Defects
Fundamentals of Alu Alu Blister Packaging Technology
To optimize an alu alu blister packaging line for zero defects, calibrate punch-to-die clearance strictly to 0.10-0.15 mm, maintain cavity corner radii of at least 1.2-1.5 mm to prevent micro-pinholes, precisely control heat sealing at 130°C-200°C and 280-320 kPa for 0.5-1.5 seconds, and integrate inline vacuum decay testing. For pharmaceutical manufacturers, contract packagers, laboratories, and equipment suppliers in Ann Arbor, those tolerances also explain why blister-line tooling, foil rolls, inspection equipment, and sealing stations must be packed, moved, and staged with the same care as any other precision industrial system.
Handle With Care Moving & Delivery does not validate pharmaceutical production lines or replace GMP engineering teams. Our role is different: we help protect sensitive commercial machinery, packed components, crates, and materials during local moves, deliveries, storage transitions, and facility reorganizations. Understanding how delicate alu alu blister packaging equipment is helps operations teams plan safer handling, reduce relocation damage, and avoid preventable startup delays after a move.
Achieving a true hermetic seal requires a deep understanding of technical specifications of alu alu blister foil. When pharmaceutical formulations degrade in ambient humidity or oxygen, cold-form foil packaging completely encloses the medicine within metallic barriers on both the cavity side and the lidding side. Standard mono-PVC films exhibit a Water Vapor Transmission Rate (WVTR) of roughly 3.1 to 9.0 g/m²/day under accelerated tropical conditions (38°C to 40°C at 75% to 90% RH). In contrast, cold-formed aluminum foil laminates achieve a WVTR of virtually 0 g/m²/day (≤0.1 g/m²/24h) and an Oxygen Transmission Rate (OTR) of ≤0.5 cm³/(m²·24h·0.1MPa), eliminating moisture absorption and hydrolytic degradation when the package is correctly formed and sealed.
Multi-Layer Material Composition and Alloy Specifications
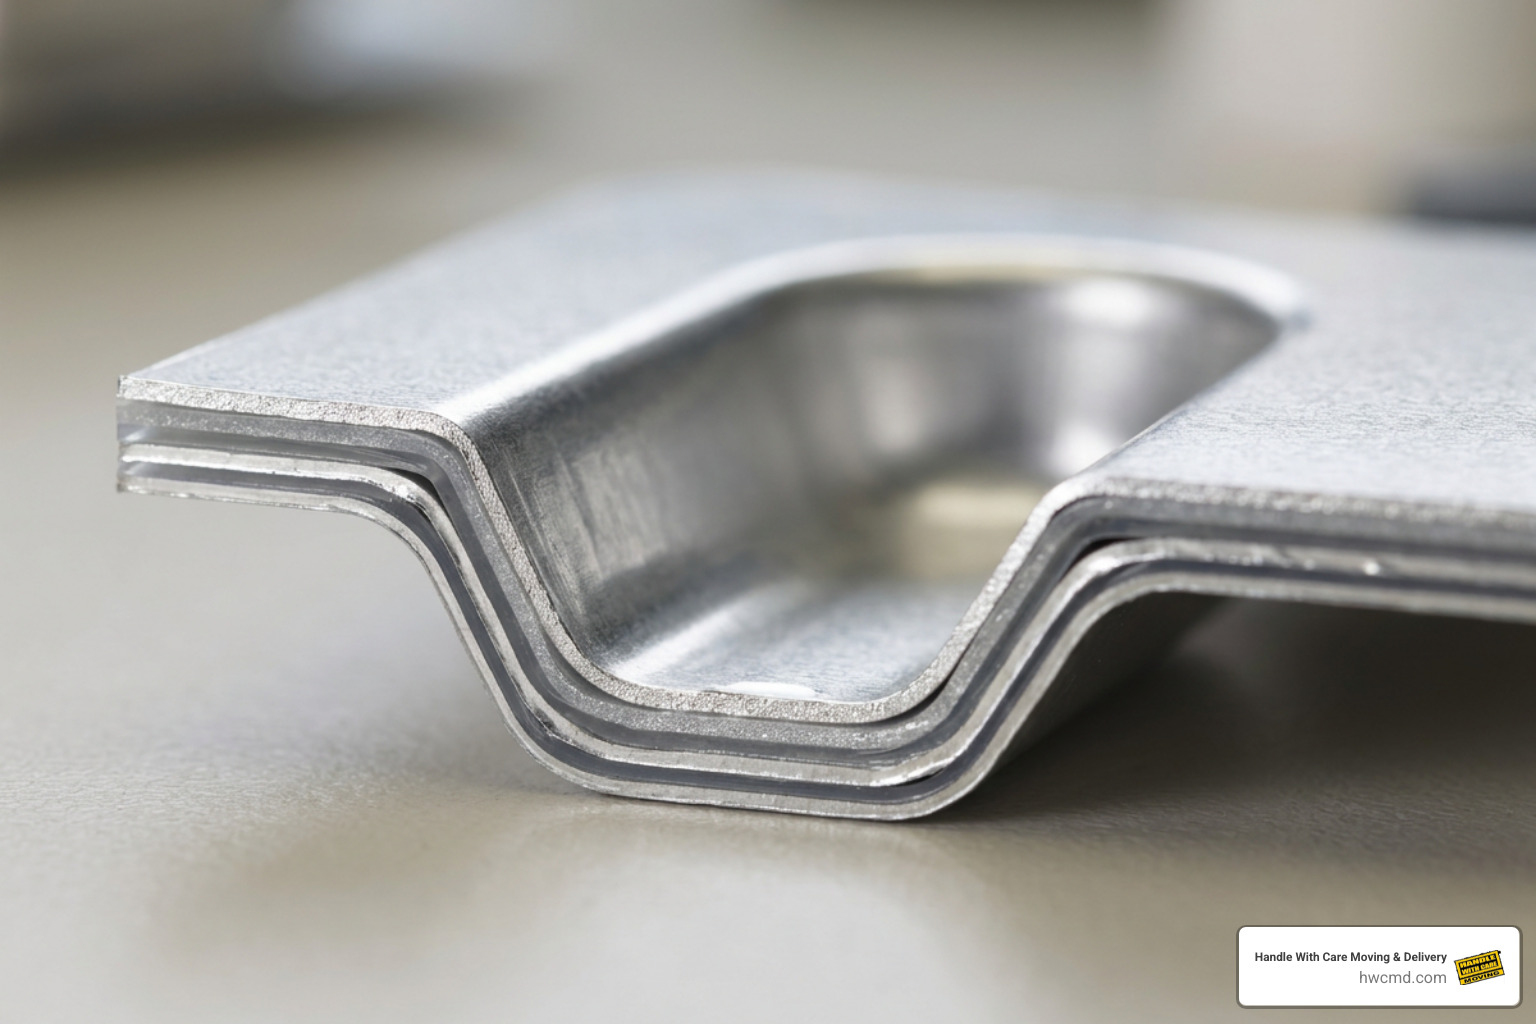
Cold-form forming foil is not a single sheet of metal. It is an engineered multi-layer composite material, typically ranging from 140 µm to 160 µm in total thickness, designed to withstand intense mechanical deformation without cracking. During facility moves or internal rearrangements, foil roll edges, forming webs, and tooling surfaces should be protected from dents, dust, and compression because small handling damage can become a production defect later.
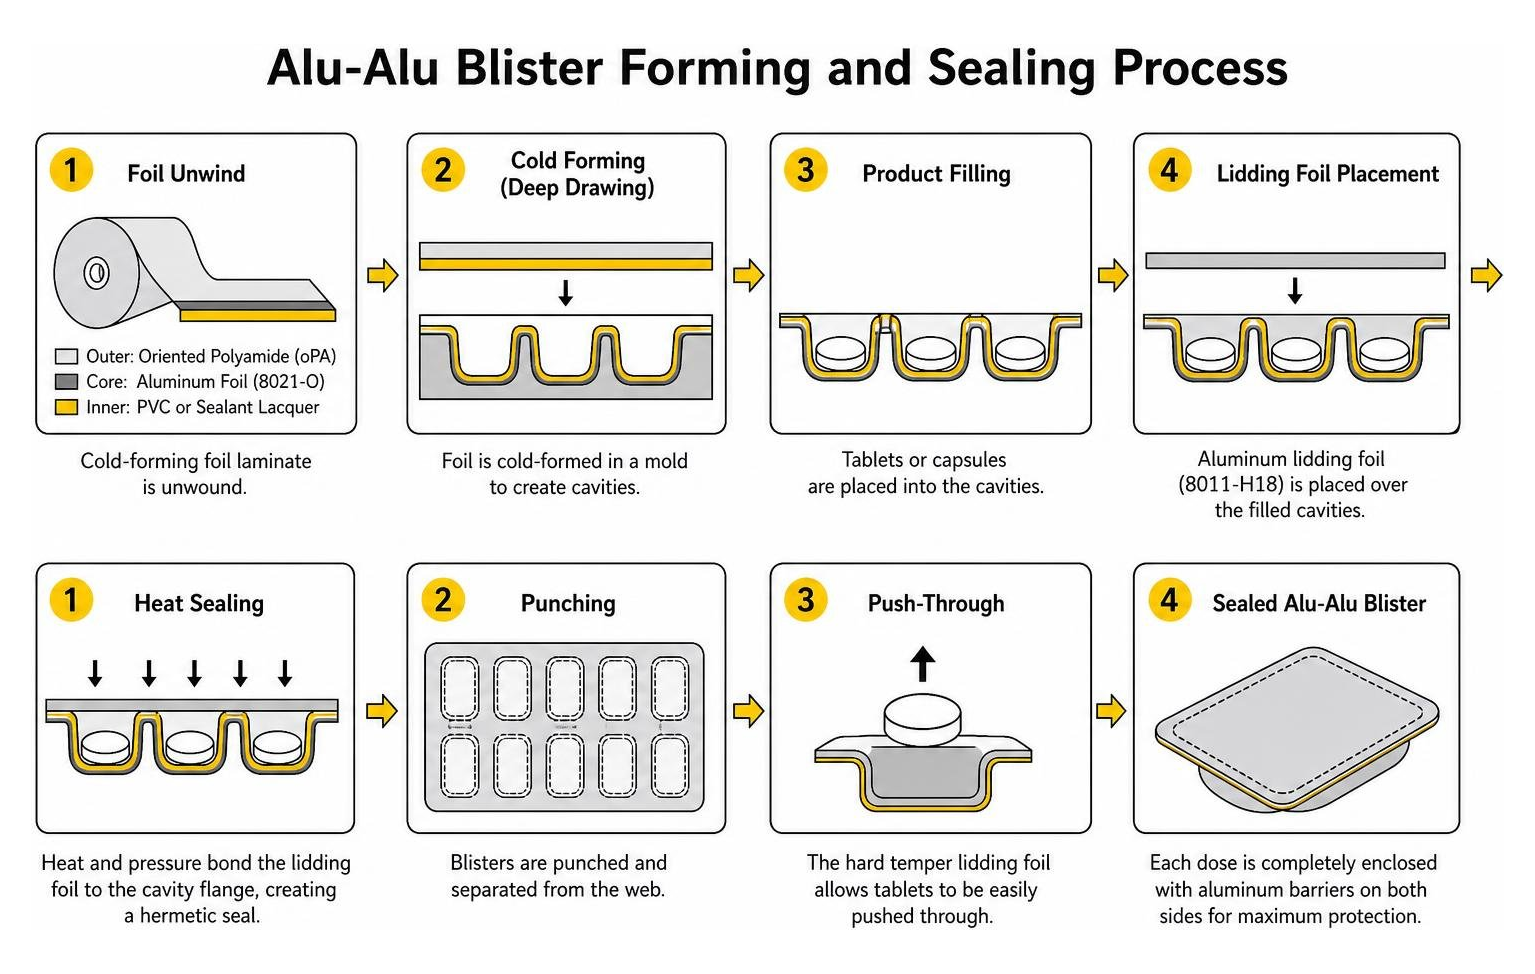
- Outer Layer – Oriented Polyamide (oPA / Nylon, ~25 µm): Serves as the outer structural backbone. It provides high tensile strength, puncture resistance, and elongation capability, evenly distributing the mechanical draw force during deep stamping.
- Core Layer – High-Purity Aluminum Foil (~45-60 µm, typically 8021-O alloy): Provides the impenetrable barrier against water vapor, oxygen, gases, and 100% of UV/visible light. The annealed “O” temper ensures maximum ductility and deep-drawing cup depth (≥4.0 mm) without tearing.
- Inner Layer – Polyvinyl Chloride or Sealant Lacquer (~60-100 µm PVC or 6-8 GSM lacquer): Direct product contact layer that bonds securely with the lidding foil during heat sealing.
For the push-through lidding foil, manufacturers typically use a hard temper 8011-H18 alloy (16-25 µm thick) with a tensile strength ≥150 MPa. This hard temper allows patients to easily press tablets through the foil backing while maintaining puncture resistance during handling and shipping.
Cold Forming vs. Thermoforming Mechanics
The difference between standard thermoformed plastic blisters and cold-formed aluminum cavities lies entirely in the underlying material physics:
- Thermoforming (PVC / PVDC / PET): Plastic film is heated above its glass transition temperature (110°C-140°C) until pliable, then shaped into cavity molds using pneumatic air pressure or vacuum suction. It cools into rigid, transparent pockets with tight, steep sidewalls.
- Cold Forming (Alu-Alu): The multi-layer foil is mechanically pressed into a die cavity at ambient room temperature using servo-driven solid punch pins, often with plug-assist support. No heat is used to shape the cavities.
Because aluminum foil deforms through mechanical plastic elongation rather than thermal softening, its crystalline lattice work-hardens under stress. Consequently, cavities cannot have sharp 90-degree corners. Instead, they require softer entry angles and larger radii, creating a slightly wider blister footprint than thermoformed plastic cards. The same sensitivity applies to the physical equipment: forming dies, punch pins, guide bushings, and inspection stations should be immobilized, cushioned, and kept square during transport so they arrive ready for engineering inspection and recommissioning.
Critical Parameters for Setting Up Zero-Defect Cold Forming Lines
Setting up a cold-forming machine like the Alu Alu Blister Packing Machine | DPP-320 Cold Forming requires fine-tuned mechanical precision. Because cold-form laminate costs 3 to 4 times more than standard PVC, running an unstable line generates expensive scrap very quickly. If a line is being delivered, relocated, or reconfigured, the move plan should protect the same alignment-critical areas that process engineers later calibrate: forming stations, sealing dies, feeders, unwind shafts, control cabinets, inspection modules, and spare tooling.

Eliminating Micro-Fissures and Pinholes in Alu Alu Blister Packaging
The most common failure on cold-forming lines is the formation of micro-pinholes at the corners and base of the blister pocket. Aluminum foil thins down from ~60 µm to 40-45 µm during deep drawing. If tooling tolerances are off, this stretching exceeds the alloy’s shear limit. Relocation-related impacts can make those problems worse by nicking punch edges, shifting guide components, or bending shafts that previously ran true.
To prevent pinhole micro-fractures after installation or relocation:
- Increase Corner Radii: Never design cavity corners with sharp edges. Maintain a minimum corner radius of 1.2 mm to 1.5 mm to allow smooth laminate flow. Protect punches and dies in padded, labeled containers so polished radii are not chipped during handling.
- Calibrate Die Clearance: Maintain punch-to-die clearance strictly between 0.10 mm and 0.15 mm. Excessive play causes foil wrinkling, while tight clearances pinch and shear the metal barrier. After a move, engineering teams should verify clearances before production restart.
- Control Draw Depth Ratios: Limit maximum forming depth to 8-12 mm depending on pocket volume. Tooling should use polished Teflon or hardened steel plug-assist tips to minimize frictional grab on the nylon layer. Spare tips and change parts should be packed so contact surfaces cannot rub against one another.
- Maintain Servo Tension: Use closed-loop servo unwinds with dancer arms to control web tension within ±5%, preventing uncontrolled foil stretching before the stamping stroke. During transport, unwind assemblies and dancer arms should be secured against free movement.
Heat Sealing Temperature, Pressure, and Dwell Time Optimization
A hermetic blister is useless if the seal between the forming cavity and the lidding foil fails. Sealing cold-form foil requires activating the inner PVC or heat-seal lacquer layer without overheating the substrate. When sealing modules are moved, heater plates, thermocouples, pneumatic connections, hydraulic lines, and PID control wiring should be protected from strain and labeled for efficient recommissioning.
- Temperature Mapping: Maintain sealing temperatures between 130°C and 200°C (commonly calibrated to 145°C-160°C ±3°C for lacquer activation). Use multi-zone PID controllers to keep thermal variation across wide dies under ±5°C.
- Dwell Time & Pressure: Set dwell times between 0.5 and 1.5 seconds at hydraulic/pneumatic pressures of 280 to 320 kPa. Excessive pressure crushes the formed pockets, while insufficient pressure causes micro-channel leaks at pocket perimeters.
- Seal Strength Targets: Achieve an ASTM F88 seal peel strength of ≥7.0 N/15mm (ideally 12-18 N/15 mm) to verify that the card will not delaminate during transit.
For moving and delivery teams, these numbers are a reminder that blister equipment is not just heavy freight. It is precision machinery. Good pre-move documentation, careful loading, protective padding, shrink wrap where appropriate, and controlled placement reduce the chance that a physical move becomes the hidden cause of later packaging defects.
Quality Control and Failure Prevention Protocols
Running high-barrier cold form technology demands strict cleanroom protocols. Maintaining packaging area relative humidity below 30% to 40% RH prevents ambient moisture from being trapped inside the cavity before sealing. During a facility move or equipment delivery, the same mindset should guide logistics planning: keep exposed tooling clean, keep sensitive parts covered, avoid uncontrolled storage conditions, and separate production-contact components from ordinary shop freight.
Non-Destructive Inspection for Alu Alu Blister Packaging Defects
Because aluminum is 100% opaque, conventional optical vision cameras cannot check pocket fill levels or inspect tablets through the cavity base. To maintain total quality control:
- ASTM F2338 Vacuum Decay Testing: Inline or benchtop instrumented vacuum chambers detect pressure rises caused by sub-micron pinholes or channel leaks, detecting defects down to ≥0.5 kPa pressure variations.
- Inline X-Ray Inspection: High-speed X-ray sensors verify product presence, tablet integrity, and correct dosing through the opaque metal foil without slowing line speeds.
- High-Voltage Pinhole Detection: Electrostatic testing detects minute discontinuities in the non-conductive polymer layers over the conductive aluminum core.
Inspection equipment is also sensitive cargo. X-ray units, vacuum decay chambers, high-voltage testers, control screens, and data terminals should be moved with appropriate padding, upright orientation where required, cable protection, and clear labeling so validation teams can reconnect and test them efficiently.
Tooling Maintenance and Validation Procedures
Cold-forming lines must follow rigorous validation lifecycles (DQ, IQ, OQ, PQ) in compliance with WHO GMP TRS 961 Annex 6 and 21 CFR Part 11 electronic batch records.
Preventive maintenance should include inspecting forming punch guide bushings every 2 million strokes, replacing bushings if lateral play exceeds 0.05 mm, and measuring incoming foil thickness with eddy-current gauges (±1 µm accuracy) to eliminate sub-gauge foil batches.
Before moving a blister line, manufacturers should inventory forming tools, change parts, spare bushings, sensors, and documentation. After the move, qualified personnel should perform the required inspection and validation steps before releasing the equipment for production. Handle With Care Moving & Delivery can support the physical moving, packing, delivery, and placement side of that process while the pharmaceutical quality team retains responsibility for GMP release.
Alu-Alu vs. Alternative Blister Barriers: Performance and Economic Trade-offs
Choosing the right barrier material requires balancing pharmaceutical shelf-life stability against overall production and shipping costs. Just as picking the best way to pack dishes for shipping safely requires choosing strong cushioning for fragile items, protecting hygroscopic formulations requires matching the packaging material to climate risks. The same practical logic applies when moving packaging equipment or materials: the more sensitive and costly the item, the more important it is to use the right protection, handling sequence, and load plan.
Barrier Integrity and Shelf-Life Performance
| Material Specification | WVTR (g/m²/day @ 38°C, 90% RH) | OTR (cm³/m²/day @ 23°C) | Light Barrier | Relative Unit Material Cost | Typical Primary Applications |
|---|---|---|---|---|---|
| Standard Mono PVC (250 µm) | 3.0 – 9.0 | ~20.0 | None (Clear) | Baseline (1.0x) | Stable OTC tablets, multivitamins |
| Duplex PVC / PVDC (60-120 gsm) | 0.9 – 2.8 | 0.5 – 1.0 | Low to None | 1.5x – 2.0x | Mildly hygroscopic solid doses |
| ACLAR / PCTFE Laminate | 0.06 – 0.40 | ~5.0 | Low to None | 2.5x – 3.0x | Moisture-sensitive drugs needing transparency |
| Cold-Form Alu-Alu (OPA/Al/PVC) | ≈ 0.00 (≤0.1) | ≤0.5 | 100% Opaque | 3.0x – 4.0x | Beta-lactam antibiotics, effervescents, PPIs |
For medications distributed in hot and humid tropical markets (ICH Climate Zone IVa/IVb: 30°C/75% RH up to 40°C/75% RH), cold-form foil prevents active ingredients from hydrolyzing, gaining water mass (1-8%), or degrading chemically over a 24-month stability lifecycle when the full packaging system is correctly designed, sealed, stored, and transported.
Total Cost of Ownership and Recyclability Challenges
While alu-alu packaging costs 25% to 50% more per finished pack than thermoformed PVC, it protects against multi-million-dollar batch recalls for unstable drugs. However, cold-form cards require larger cavity spacing (5-10 mm web bridges), resulting in a larger physical footprint. This slightly increases outer folding carton volumes and secondary shipping bulk.
From a sustainability perspective, pure aluminum is infinitely recyclable. However, separating bonded OPA/Aluminum/PVC multi-layer laminates requires specialized industrial delamination recycling streams.
For companies handling finished blister packs, foil rolls, or blister-line assets, total cost of ownership also includes avoidable damage during internal moves, delivery, staging, and storage. Larger footprints mean more cartons, more pallet positions, and more opportunities for corner crush, vibration, or misplacement. Careful packing and delivery practices help protect both the pharmaceutical product and the capital equipment used to make it.
Frequently Asked Questions About Cold Form Blister Lines
What causes pinholes in cold-formed blister cavities?
Pinholes typically occur when the mechanical draw depth exceeds the foil’s elongation limit, when punch pin corner radii are too sharp (<1.2 mm), when die clearances pinch the web, or when low-ductility aluminum alloy grades, such as non-annealed foils, are used instead of soft 8021-O temper material. Physical handling damage to tooling can also contribute, which is why punches, dies, and change parts should be protected carefully during equipment moves.
How does alu-alu packaging compare to PVC/PVDC in tropical climates?
In WHO Climate Zone IVb conditions (30°C/75% RH sustained), standard PVC and light PVDC films allow ambient moisture vapor to permeate into the pocket over 6 to 12 months. This moisture ingress can cause effervescent tablets to gas off and antibiotics to degrade. Cold-form alu-alu provides a complete physical barrier with a WVTR near zero, maintaining drug potency for 24+ months when the packaging process, storage, and distribution chain are properly controlled.
What inspection methods work best for opaque aluminum blister packs?
Because cameras cannot see through opaque aluminum foil, packaging lines rely on ASTM F2338 non-destructive vacuum decay leak testing, high-voltage spark testing, inline X-ray imaging for broken or missing tablets, and laser headspace analysis to ensure complete container closure integrity. These inspection stations should be treated as sensitive electronic and mechanical equipment during relocation or delivery.
Conclusion
Mastering cold-form blister operations is all about precision engineering: matching 8021-O alloy formability with exact tool clearances, stable multi-zone heat sealing, and sensitive inline leak detection. When line parameters are dialed in, manufacturers can reduce moisture degradation risk and deliver long-lasting shelf stability across global climate zones.
That same zero-defect mindset matters before the line ever restarts after a move. Tooling, foil rolls, inspection systems, control panels, and sealing modules all need careful packing, clear labeling, stable transport, and thoughtful placement so pharmaceutical engineers can complete alignment checks and validation without avoidable handling damage.
At Handle With Care Moving & Delivery, our daily mission revolves around absolute protection, careful handling, and dependable service. Whether we are moving heavy, sensitive commercial machinery, handling high-end freight, or providing full-service residential packing across Ann Arbor, Michigan, we believe every valuable item deserves thoughtful care. When you want reliable logistics backed by transparent 15-minute pricing, complimentary protective materials, and dedicated service, explore our professional packing services materials to keep your items safe from start to finish.